


What is Xylene?
Xylene (molecular formula:  ) is one of the most important aromatic hydrocarbon basic chemical raw materials in the petroleum refining and chemical industry. Commercially, it is available as mixed xylene and three monomer isomers: o‑xylene, m‑xylene and p‑xylene.
At ambient temperature, xylene features stable chemical properties and resists spontaneous polymerization and decomposition. It exhibits typical chemical reactivity of aromatic hydrocarbons and can undergo sulfonation, nitration, oxidation and alkylation reactions, hence being widely applied in diverse organic synthesis processes. Different isomers show distinct application scenarios:
Mixed xylene: A general‑purpose industrial solvent extensively used in coatings, printing inks and cleaning industries.
p‑Xylene (PX): A core feedstock for the production of PTA and polyester chemical fibers.
o‑Xylene: Used for manufacturing phthalic anhydride, plasticizers and other fine‑chemical products.
Basic Physicochemical Parameters of Xylene
|
Item |
Technical Parameter |
|
Chinese Name |
Xylene, Mixed Xylene, Dimethylbenzene |
|
English Name |
Xylene (Mixed Xylene) |
|
CAS‑RN (Mixed Xylene) |
1330‑20‑7 |
|
CAS‑RN (o‑Xylene) |
95‑47‑6 |
|
CAS‑RN (m‑Xylene) |
108‑38‑3 |
|
CAS‑RN (p‑Xylene) |
106‑42‑3 |
|
EINECS |
215‑535‑7 |
|
Molecular Formula |
|
|
Molecular Weight |
106.17 |
|
Appearance |
Colorless, transparent, free‑flowing liquid, free of turbidity and solid mechanical impurities |
|
Odor |
Mild characteristic aromatic‑hydrocarbon odor; no abnormal putrid odour |
|
Water Solubility |
Practically insoluble in water; fully miscible with ethanol, ether, acetone, esters, alkanes and most organic solvents |
|
Boiling‑Point Range (Mixed Xylene) |
136‑144 ℃ |
|
Density (20 ℃) |
0.860‑0.880 g/cm³ |
|
Closed‑cup Flash Point |
27 ℃ |
|
Explosion Limit (Volume Fraction) |
1.1‑7.0 % |
|
Auto‑ignition Temperature |
464 ℃ |
|
UN Dangerous Goods Number |
1307 |
|
pH of Aqueous Solution |
Neutral |
|
Key Properties |
Strong resin‑dissolving capacity; excellent penetration and wetting performance; uniform volatilization rate; good compatibility with multiple chemical materials |
|
Chemical Stability |
Stable under airtight ambient‑temperature storage. Contact with strong oxidizing agents is strictly prohibited, as violent oxidation reactions may be triggered. Vapors are heavier than air and tend to accumulate in low‑lying and enclosed spaces, presenting a risk of flashback. |
|
Hazard Classification |
Class 3 flammable liquid, Category B hazardous chemical; volatile irritant solvent; high‑concentration inhalation produces narcotic effects |

Industrial Production: Toluene Disproportionation‑Transalkylation Process
Production Feedstocks and Auxiliary Media
Main Feedstocks
Refined toluene: Sourced from the aromatic‑hydrocarbon extraction and rectification unit of reformate gasoline, purity ≥ 99.5 %.
C9 heavy aromatics: Mixture of trimethylbenzene isomers, a by‑product from the bottom of aromatic‑hydrocarbon unit columns.
Auxiliary Media
Recycled high‑purity hydrogen: Inhibits catalyst coking and extends catalyst service life.
Catalyst: Modified ZSM‑5 zeolite (high‑temperature resistant, shape‑selective catalysis, high activity).
Utility media: Circulating cooling water, steam, compressed air, nitrogen.
Core Chemical‑Reaction Principles
The process involves two groups of reversible main reactions. Minor side reactions occur during production and can be suppressed by adjusting process parameters.
Toluene disproportionation reaction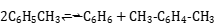
Toluene‑trimethylbenzene transalkylation (key reaction for xylene yield enhancement)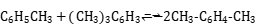
Side reactions: Hydrodealkylation (methyl group cleavage to generate methane and light benzene fractions), aromatic‑hydrocarbon cracking to form light alkanes. Higher hydrogen‑to‑hydrocarbon molar ratios and controlled temperature ranges mitigate side reactions.
Key Process Operating Conditions
|
Process Parameter |
Control Range |
Remarks |
|
Reaction Temperature |
370‑460 ℃ |
Insufficient activity at low temperature; excessive coking and more by‑products at overly high temperature. |
|
Reaction Pressure |
1.5‑3.0 MPa |
Hydro‑rich high‑pressure environment protects catalysts and lowers coking rates. |
|
Hydrogen‑to‑Hydrocarbon Molar Ratio |
4‑6:1 |
Excess hydrogen stabilizes the reaction system. |
|
Mass Hourly Space Velocity |
1.0‑1.5 h⁻¹ |
Controls feed residence time in reactor to guarantee conversion efficiency. |
|
Catalyst Service Life |
3‑5 years |
Modified ZSM‑5 zeolite |
Complete Industrial Process Flow
Feedstock Pretreatment
Toluene and C9 heavy aromatics enter buffer tanks for pressure stabilization. Filters remove solid particles, gums and trace heavy metals to prevent catalyst poisoning and equipment blockage. Feedstocks are mixed with recycled hydrogen and pre‑heated by waste heat from reactor effluent to reduce unit energy consumption.
Heating and Fixed‑bed Reaction
Materials are heated in a furnace to target reaction temperature and fed into the disproportionation reactor. Under catalysis by ZSM‑5 zeolite, disproportionation and transalkylation proceed, producing a mixture containing benzene, unreacted toluene, mixed xylene, minor C9+ heavy aromatics and light hydrocarbons.
Cooling, Gas‑Liquid Separation and Hydrogen Recycling
High‑temperature reactor effluent pre‑heats incoming feed and is cooled to ambient temperature with cooling water before entering a gas‑liquid separator. Hydrogen‑rich gas phase is desulfurized and purified, then compressed and recycled to the reactor inlet for reuse. Liquid hydrocarbons are sent to the rectification section.
Multi‑stage Rectification and Purification (core for product separation)
Light‑hydrocarbon stripper: Removes light by‑products such as methane and ethane.
Benzene column: High‑purity benzene is drawn off overhead as a by‑product for commercial sale.
Toluene recovery column: All unreacted toluene is recycled back to feed tanks for re‑reaction to improve feed utilization.
C8 aromatic‑hydrocarbon column: Yields main product high‑purity mixed xylene; recovered C9 heavy aromatics are recycled as transalkylation feedstock.
Subsequent Monomer Separation and Refining
Rectified mixed xylene can be sold directly as a commercial industrial product. Alternatively, it is sent to an adsorption‑separation unit combining simulated moving‑bed adsorption and precision rectification to isolate high‑purity o‑, m‑ and p‑xylene monomers for chemical‑fiber and fine‑chemical applications.
Process Advantages and Output Indicators
Single‑pass toluene conversion: 40 %‑50 %.
Feedstock recycling, low solid‑waste output, low energy consumption and high xylene selectivity.
Produced mixed C8 xylene achieves purity ≥ 98 %, meeting superior‑grade industrial‑product specifications.
Xylene Product Grades and Application Scenarios
Reagent‑grade xylene (laboratory use)
Classified as Analytical Reagent (AR) and Chemical Pure (CP). AR purity ≥ 99.5 %; CP purity ≥ 99.0 %. Strict impurity limits: benzene ≤ 0.1 %, toluene ≤ 0.3 %, water ≤ 0.03 %, evaporation residue ≤ 0.001 %. Used for laboratory chemical analysis and small‑scale precision synthesis.
Special high‑purity grade (industrial synthesis)
Typical example: p‑xylene for PTA plants, purity ≥ 99.8 %, isomer impurities ≤ 0.2 %, hetero‑atom impurities such as sulfur and nitrogen ≤ 0.001 %, satisfying stringent reaction conditions for polyester synthesis.
Industrial‑grade mixed xylene
High‑purity C8 aromatic‑hydrocarbon, colorless and transparent, slightly soluble in water. Widely applied as diluent for coatings and printing inks, and as industrial solvent. Some products are categorized by distillation range: superior grade with 3 ℃ distillation‑range specification; Grade I with 5 ℃ distillation‑range specification.
Xylene Industrial Chain
Xylene is a core basic chemical in the petroleum aromatic‑hydrocarbon industrial chain. China possesses large‑scale refining‑chemical units with well‑developed and complete upstream‑downstream supporting facilities.
Upstream feedstocks: Naphtha, pyrolysis gasoline, reformed aromatics, hydrogenation catalysts, aromatic‑hydrocarbon extraction solvents, industrial purified water.
Major downstream applications:
Diluting solvents for paints, coatings and printing inks
Solvents for adhesive manufacturing
Processing auxiliaries for rubber and plastics
Industrial cleaning solvents
Feedstock for PTA‑polyester chemical‑fiber production (p‑xylene)
Intermediates for phthalic‑anhydride and plasticizer production (o‑xylene)
Fine organic synthesis for dyestuff and pharmaceutical industries
Storage, Transportation and On‑site EHS Safety Specifications
Storage Requirements
Store in explosion‑proof hazardous‑chemical warehouses; warehouse temperature ≤ 30 ℃. Keep away from heat sources, open flames, static electricity and strong oxidizing agents.
Keep containers fully sealed to prevent volatilization and water ingress. All electrical equipment inside warehouses shall be explosion‑proof and anti‑static.
Store in separate designated zones; co‑storage with strong oxidizing agents, strong acids or strong bases is prohibited.
Maintain forced ventilation. Equip with sand, absorbent cotton, compatible fire‑fighting equipment and leakage emergency containment facilities; perform regular inspections.
Transportation Regulations
Comply with UN1307 dangerous‑goods transportation regulations. Transport companies, drivers and escorts shall hold valid hazardous‑chemical operation qualifications.
Ensure tight and intact packaging; protect from sunlight, rain and leakage.
Mixed loading with oxidizing agents, strong acids or food‑grade goods is prohibited.
On‑site Operating Specifications
Eliminate all ignition sources in work zones and maintain forced ventilation.
Personal protective equipment: Organic‑vapor gas mask, safety goggles and solvent‑resistant nitrile gloves.
In case of skin or eye contact: Rinse immediately with large volumes of running water continuously and seek medical attention when necessary.
Leak handling: Isolate and eliminate ignition sources as priority. Contain and absorb spilled liquid with sand or absorbent cotton. Do NOT rinse directly with water, to avoid liquid spreading and enlarged hazard scope.
Frequently Asked Professional Questions (FAQ)
Q: How to choose between mixed xylene and high‑purity single‑component xylene?
A: They share identical parent chemical structures, differing mainly in component purity, impurities and applicable scenarios.
Mixed xylene: Mixture of o‑, m‑ and p‑xylene isomers, cost‑effective with excellent solvent dissolving and compatibility performance. Suitable for coatings, printing inks, industrial cleaning and general‑purpose dilution.
High‑purity monomeric xylene (≥ 99.5 %): Extremely low isomer impurities with predictable and controllable chemical reactions. Used for directional fine‑chemical synthesis such as polyester and phthalic‑anhydride production.
Q: How to select among toluene, xylene and trimethylbenzene?
A: Core selection indicators: boiling point, volatilization rate and coating‑process requirements.
Toluene: Low boiling point and fastest volatilization. Suitable for fast‑drying and thin‑film coating systems.
Xylene: Moderate and balanced boiling point and volatilization rate, balancing dissolving power and film‑forming performance. The preferred universal option for most baking finishes, anti‑corrosion coatings and printing‑ink industries.
Trimethylbenzene: Higher boiling point and slower volatilization. Suitable for high‑solid‑content, thick‑film, slow‑drying formulations requiring high weather resistance.
Q: What are the advantages of China's xylene industry?
A: China's xylene industry is supported by mature refining, reforming and hydrotreating processes. It features a complete industrial chain and the world's leading production capacity. The isomerization and purification technology is well-established and stable, enabling bulk supply of a full range of products including industrial grade, refined grade and high-purity single-component grades. The product quality meets international standards with remarkable cost advantages, fully catering to the essential demands of China's core sectors such as coatings, chemicals and chemical fibers. Leveraging China's massive xylene market advantages, 7DCHEM combines dual-warehouse services in Poland to serve chemical procurement requirements in Central and Eastern Europe as well as Ukraine.


